

 English
 عربى
 简体中文
 +86-0573-89103923 / +86 182 6841 1181
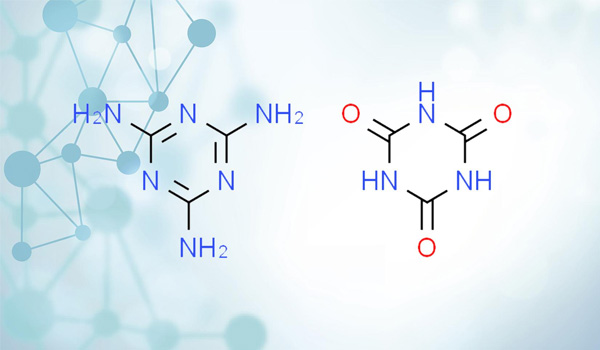
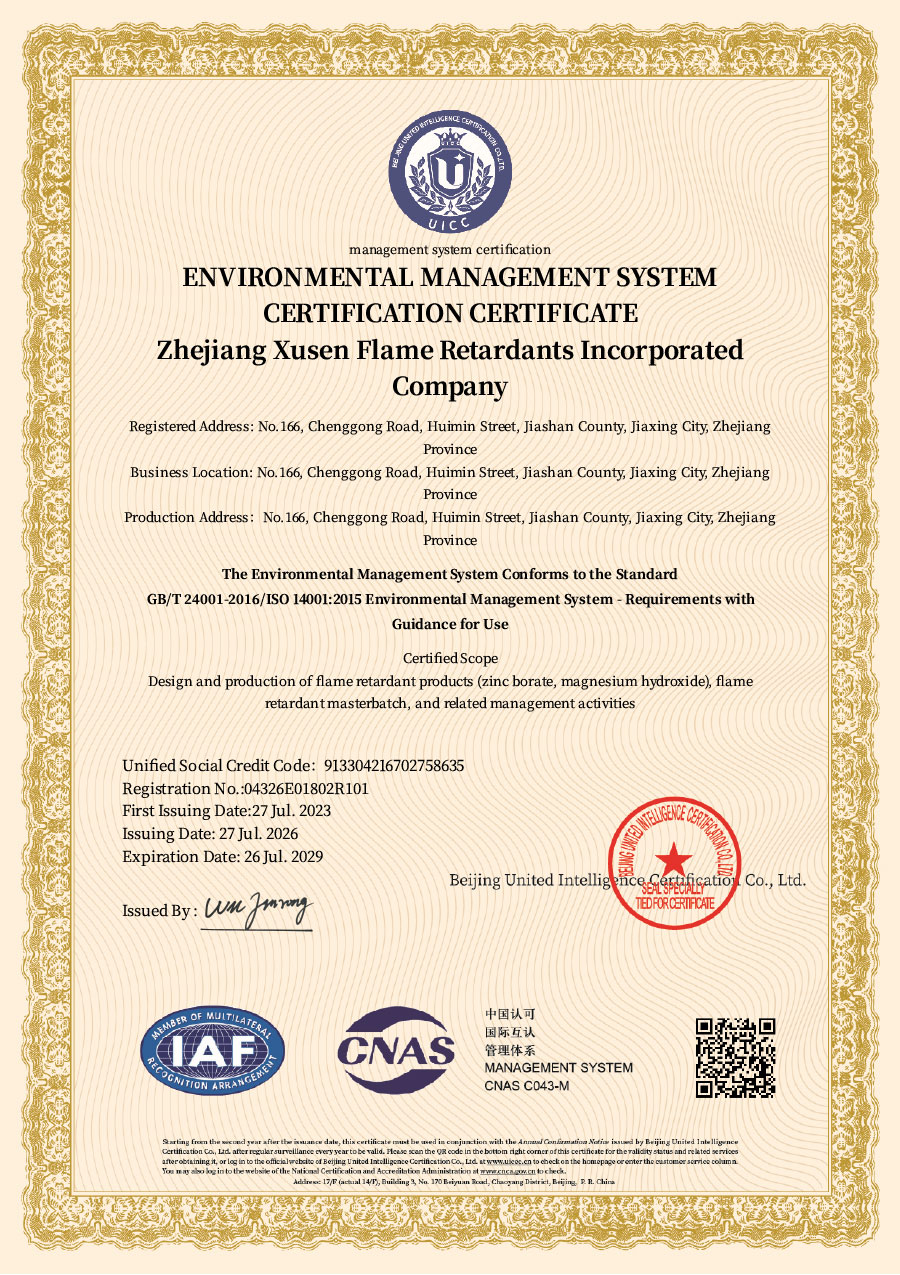
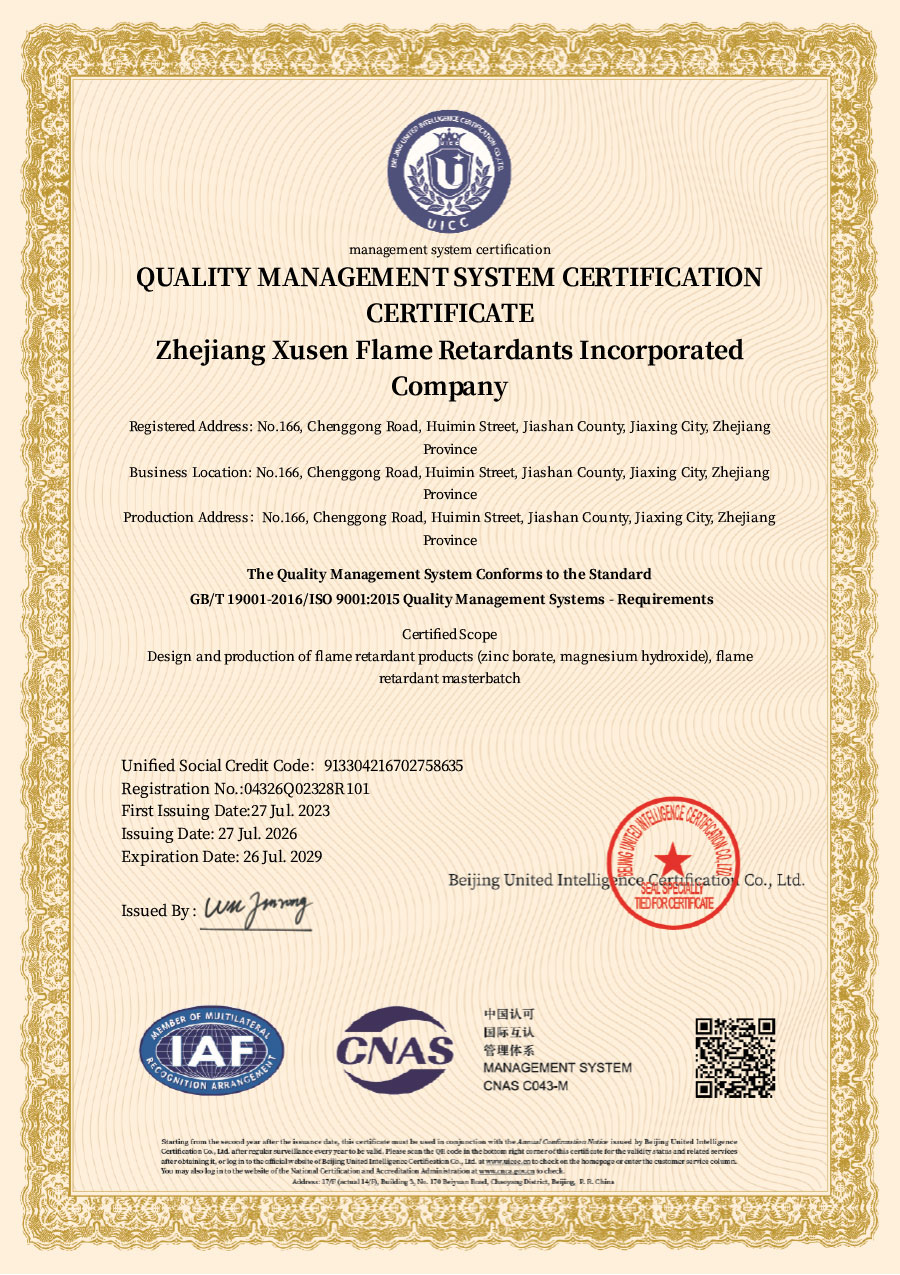
Zhejiang Xusen Flame Retardants Incorporated Company is a Functional additives for PA manufacturer operating from two production bases in Jiashan, Zhejiang and Juancheng, Shandong. The range covers nucleating agents, flowability modifiers and thermal stabilizers developed for PA6, PA66, PA12, PPA and the toughened and fibre-reinforced compounds built on those resins.
These products are not flame retardants. They are the additives that determine whether a nylon part fills completely, releases from the tool, holds its dimensions after moulding and survives the heat history of compounding and injection. We supply them as standalone grades and adapt the formulation to the process window and property target of the compound they are going into.
The Functional Additives for PA Range
Three product families cover the most common functional gaps in nylon compounding and moulding. Each is supplied as a free-flowing powder, with a masterbatch format available through our functional additives masterbatch range where dust control and gravimetric feeding accuracy matter.
| Product | Primary function | PA matrices | Application fit |
|---|---|---|---|
| XS-CH-101 Nucleating Agent For PA | Accelerates crystallisation, refines crystal structure, shortens cooling time and improves dimensional stability and surface finish | PA6, PA66, PA12, PPA; unfilled, glass-filled and mineral-filled grades | Injection-moulded connectors, housings, brackets, gears and thin-wall electrical parts |
| XS-LU-403 Flowability Modifier For PA | Reduces melt viscosity, improves cavity fill, weld-line quality and surface appearance at lower injection pressure | PA6, PA66, PPA; glass-fibre and mineral reinforced grades | Long-flow parts, thin-wall connectors, multi-cavity tools and structural fibre-filled components |
| XS-KY-300 Thermal Stabilizer For PA | Protects the melt against thermo-oxidative degradation during compounding and moulding, and supports heat-ageing performance | PA6, PA66, PPA; reinforced and impact-modified grades | Under-hood parts, high-temperature electrical components, extrusion and high-shear compounding |
The three grades are designed to work as a package. A glass-filled PA66 connector that has to fill a long, thin flow path at a short cycle time usually needs flow modification and nucleation together, with thermal stabilisation sized to the melt temperature and residence time of the barrel.
Where the Range Fits in the PA Process
Nucleation and cycle time
PA crystallises slowly in the tool, and the cooling phase often sets the floor on cycle time. A nucleating agent raises the crystallisation rate and produces a finer, more uniform crystal structure, which shortens the time the part must stay in the mould and reduces post-mould shrinkage and warpage. The effect is most visible in thin-wall electrical parts and in precision components where dimensional tolerance is tight.
Flow and cavity fill
Glass fibre and mineral fillers raise melt viscosity and make long flow paths difficult to fill without pushing injection pressure and melt temperature higher. A flowability modifier lowers the effective viscosity of the melt, improving cavity fill, weld-line quality and surface appearance while allowing the machine to run at a lower pressure. It is used in multi-cavity tools, thin-wall connectors and structural parts with long flow-to-thickness ratios.
Thermal protection through compounding and moulding
Nylon is sensitive to thermo-oxidative degradation. Every pass through an extruder or an injection barrel consumes part of the polymer's thermal budget, and the damage shows up as discolouration, molecular weight loss, surface defects and reduced mechanical performance. A thermal stabilizer protects the melt during compounding and moulding and supports the heat-ageing performance of the finished part in under-hood and high-temperature electrical applications.
Material and Part Considerations
Additive selection follows the compound, not the other way round. The variables that change the answer most often are:
- Polymer type and viscosity — PA6, PA66, PA12 and PPA differ in melting point, crystallisation behaviour and processing window, and a grade that suits PA6 may not suit a high-melting PPA.
- Reinforcement — glass fibre and mineral fillers change dispersion behaviour, feeding point and the level of flow modification required.
- Toughener system — impact-modified nylons interact with nucleation and stabilisation differently from unmodified grades.
- Wall thickness and flow length — thin walls and long flow paths put the emphasis on flow and nucleation; thick sections put it on cooling uniformity and shrinkage.
- Colour and surface requirements — additives that disperse poorly show up as black specks, white points or streaks on visible parts.
- Regrind and moisture — recycled content and residual moisture raise the thermal load and change the stabilisation requirement.
- End-use environment — continuous service temperature and heat-ageing targets set the level of thermal protection.
Setting the Working Addition Level
There is no single addition level that applies across the range. The working figure is established from the base polymer, the reinforcement and toughener package, the processing method, the melt temperature and residence time, and the property balance the part has to meet. We start from the closest existing grade and adjust from there.
Where the compound already carries a flame-retardant system, we check compatibility before recommending a loading. MCA, ammonium polyphosphate and composite phosphorus-nitrogen systems each interact differently with nucleating agents and stabilizers, and the additive package has to be balanced as a whole rather than optimised one component at a time.
Manufacturing, Capacity and Quality
Production runs across two bases in Jiashan, Zhejiang and Juancheng, Shandong, with an annual capacity of 12,000 tons that continues to expand. Both sites operate under the ISO 9001-2015 quality management system, with in-house production workshops, warehouses and complete production and quality inspection equipment.
- Zhejiang provincial-level scientific research laboratory for flame-retardant and functional additive development.
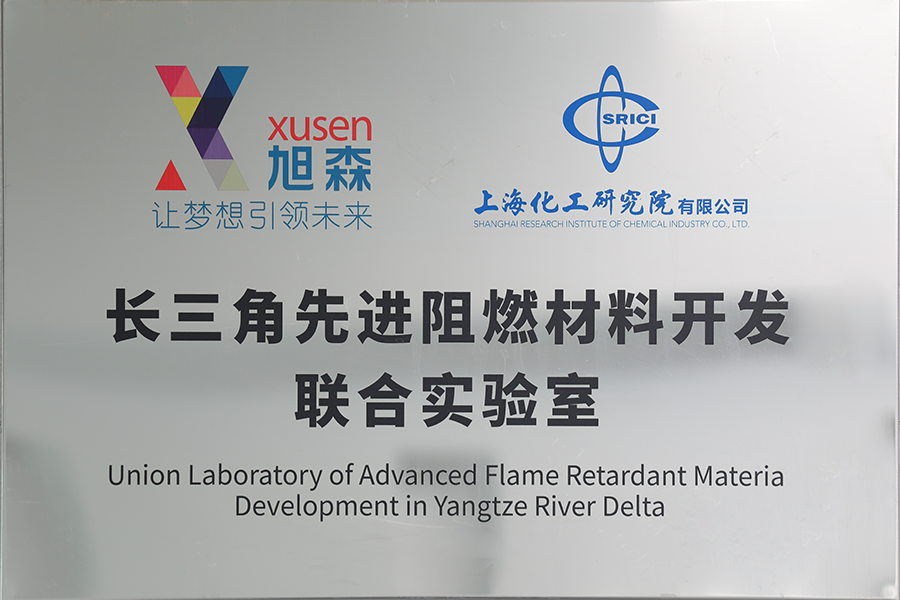
- Joint laboratory with the Shanghai Institute of Chemistry for advanced flame-retardant materials.
- Advanced light industry flame retardant engineering technology research centre established with Beijing Technology and Business University, Shandong Haihuai Institute and Shandong Brothers.
- Invention and utility model patents, plus participation in the formulation of national and industry standards.
Compliance and Documentation
Our products comply with the requirements of the WEEE, RoHS and EUP directives, and our MCA and APP grades are REACH registered. RoHS test reports are held for our flame-retardant systems for PA, and halogen test reports for MCA. The same environmental policy governs the functional additive range.
Documentation issued with a delivery covers the safety data sheet and the compliance statements that apply to the delivered grade, so incoming inspection can be matched to the lot received.
Customization, Packaging and Delivery
We make adaptive improvements to the standard grades according to user requirements, so the product better matches the process and the finished part. That can mean adjusting the carrier, the particle size distribution or the surface treatment to suit a specific feeding system or dispersion requirement.
Packaging format, pallet configuration and delivery scope are agreed at order confirmation so the material arrives in the handling format the plant uses. Storage guidance covering dry conditions, sealed packaging and controlled moisture pickup is provided with the shipment.
Information We Use to Configure Your Solution
A proposal is built from the working point, the material and the production target. The following inputs let us select the grade and set the starting addition level without a round of guesswork.
| Information | What it determines |
|---|---|
| Base polymer and grade (PA6, PA66, PA12, PPA), viscosity or MFI | Carrier compatibility and expected crystallisation behaviour |
| Reinforcement type and loading | Dispersion behaviour, feeding point and flow modification requirement |
| Toughener or impact modifier type and level | Interaction with nucleation and thermal stabilisation |
| Processing method: injection moulding, extrusion or fibre spinning | Supply form and the thermal load the additive must survive |
| Melt temperature, residence time and shear level | Thermal stabiliser selection and starting loading |
| Tool geometry: wall thickness, flow length, gate and weld-line position | Whether a flowability modifier is needed and at what level |
| Target cycle time and dimensional tolerance | Nucleating agent selection |
| Property targets: tensile, impact, HDT, surface and colour | Balance point of the additive package |
| Existing flame-retardant system in the compound | Compatibility check with MCA, APP or composite systems |
| Regrind ratio and moisture control | Stabilisation level and drying guidance |
| Regulatory target and documentation needs | Compliance statements issued with the order |
| Annual volume, packaging and handling | Supply format and delivery scope |
Technical Support and Serviceability
Support continues past the first delivery. We work with the customer's process team during the trial, review the results against the target property set, and adjust the grade or the loading where the data calls for it.
- Trial support for compounding and moulding, including guidance on feeding point and dispersion.
- Compatibility checks against existing flame-retardant and stabiliser packages.
- Storage and moisture-control guidance to protect the additive before use.
- Process and technical support as part of the supply relationship.
Frequently Asked Questions
Which PA resins do your functional additives work in?
The range is formulated for PA6, PA66, PA12, PPA and other nylon grades, including the toughened and fibre-reinforced modified materials built on them. Because melting point, crystallisation rate and processing window differ across these resins, we select the grade against the specific polymer rather than applying one product across the family.
Can a nucleating agent and a flowability modifier be used in the same compound?
Yes. The two work on different parts of the process — crystallisation and melt viscosity — and are frequently combined in glass-filled grades where a long flow path has to fill at a short cycle time. We check the interaction between the components and set the ratio against the trial result rather than treating them as independent additions.
Do these additives change the flame retardancy of the compound?
They are functional additives, not flame retardants. In compounds that already contain MCA, ammonium polyphosphate or a composite phosphorus-nitrogen system, the functional package is checked for compatibility with the flame-retardant system so that flame-retardant performance and the mechanical balance are not disturbed.
How do you decide the addition level for a new compound?
From the base polymer, the filler and toughener package, the processing method and the property target. We start from the closest existing grade, propose a starting level, and confirm it during a joint trial on your line. The final figure is the one that meets the property target at the lowest cost in the compound.
Can you adapt a grade to our process?
We make adaptive improvements to the standard products according to user requirements, covering carrier, particle size distribution and surface treatment where the feeding system or dispersion behaviour calls for it. The starting point is always the standard grade, so the change stays measurable.
What do you need from us to prepare a quotation?
The polymer and grade, reinforcement and toughener package, processing method, melt temperature and residence time, tool geometry, property targets, any existing flame-retardant system, annual volume and the packaging format you use. With those inputs we can select the grade, propose a starting addition level and set the delivery scope.