

 English
 عربى
 简体中文
 +86-0573-89103923 / +86 182 6841 1181

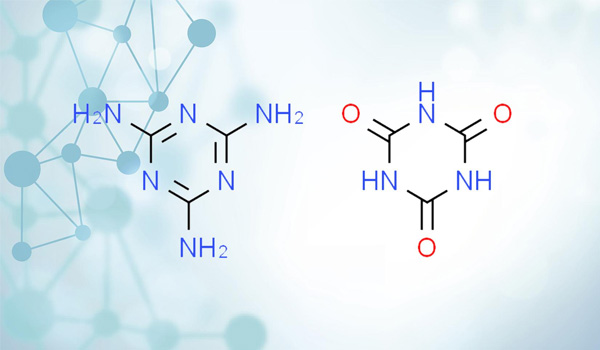
Zhejiang Xusen Flame Retardants Incorporated Company is a Melamine cyanurate(MCA)manufacturer in China, producing the XS-MC series as a nitrogen-based, halogen-free flame retardant for engineering plastics, wire and cable compounds, rubber, coatings and textile backcoatings. MCA is the single-substance grade in our portfolio with the highest nitrogen content and the cleanest combustion chemistry, and it sits alongside Ammonium polyphosphate (APP) and our composite systems where a phosphorus-nitrogen balance is the better answer.
At a glance: CAS 37640-57-6 · C6H9N9O3 · white crystalline powder, typically 1–5 μm · weakly acidic, practically insoluble in water · stable to roughly 300–320 °C, decomposing near 350 °C · REACH registered · supplied as XS-MC-15 (wet synthesis) and XS-MC-10/25/50 (dry synthesis).
The XS-MC Range: Two Synthesis Routes, One Product Family
MCA is synthesized from melamine and cyanuric acid into a 1:1 adduct. The result is a colourless, odourless, non-toxic white crystalline powder that is difficult to dissolve in water but soluble in ethanol, formaldehyde and similar solvents. Its chemical and thermal stability is what allows it to survive compounding temperatures in polyamide and polyester without pre-decomposing in the barrel.
We run two synthesis routes so that the grade can be matched to the polymer and the process rather than the other way round. The wet route gives the XS-MC-15 Series; the dry route gives the XS-MC-10/25/50 Series. Both are REACH registered and both are available with our surface modification treatment.
| Series | Synthesis route | Typical polymer fit | Role in the formulation |
|---|---|---|---|
| XS-MC-15 Series | Wet synthesis | PA6 and PA66 compounds, PBT, wire and cable insulation, electronic and electrical mouldings | Primary nitrogen-based flame retardant; gas-phase dilution with char formation from the polyamide itself |
| XS-MC-10 / 25 / 50 Series | Dry synthesis | PP compounds, rubber, cable materials, adhesives, coatings, carpet and fabric backcoatings | Flame retardant component, normally paired with a phosphorus-nitrogen or char-forming partner in non-charring polymers |
| Surface-modified variants | Applied to either series | Thin-wall parts, high-speed extrusion, compounds sensitive to surface appearance | Improves dispersion and reduces black and white specks in the finished article |
How MCA Behaves in a Burning Polymer
When a polymer containing MCA burns, the MCA decomposes and releases a large volume of non-combustible nitrogen-containing gas. That gas dilutes oxygen and radical species in the flame zone, while the residue builds a foam layer on the polymer surface that insulates the substrate from heat and oxygen and blocks further combustion. The action is physical and gas-phase rather than a halogen radical trap, which is why MCA can replace halogen-containing flame retardants in many application fields with a better environmental and smoke profile.
The practical consequence is that MCA is a dilution-type mechanism and needs a polymer that can form char. In polyamides the polymer supplies that char. In polyolefins it does not, so MCA is normally used with a phosphorus-nitrogen or intumescent partner rather than on its own.
Application Fit by Polymer and Process
Polyamide — PA6, PA66 and reinforced grades
MCA is employed commercially as a flame retardant for polyamides and terephthalates. In unfilled and mineral-filled PA6 and PA66 it works largely in the gas phase while the polyamide provides the char, which makes it a natural fit for electrical connectors, circuit-breaker housings, terminal blocks, switchgear and under-hood automotive parts. In glass-fibre reinforced polyamide, MCA alone frequently needs a synergist to reach the target rating; in those cases we propose a Composite flame retardant for PA built around the same chemistry.
Polypropylene, PBT and other thermoplastics
In PP compounds, MCA is used where heat resistance and flame retardancy are both required, such as automotive parts and electrical components. Because PP does not char readily, the formulation normally carries an additional char-forming component. PBT is a more direct fit: MCA can be incorporated into PBT resins used in electronics, automotive and electrical enclosures, where the polyester backbone supports char formation in the same way polyamide does.
Rubber, cable, coatings, adhesives and textiles
Beyond thermoplastics, MCA is used in rubber formulations where flame retardancy is critical, including wire and cable insulation, automotive parts and construction materials. In coatings and adhesives it raises flame retardancy without compromising the adhesive or coating properties, which suits building materials and electronics. In textiles it is applied through fabric coatings for upholstery, carpets and protective clothing, and it also appears in insulation foams, paints and composite building materials.
Selection Variables That Decide the Grade and the Loading
The variables below are the ones that move a formulation from a laboratory result to a stable production compound. They also define what we need from you before we can commit to a grade and a loading window.
- Loading level — the balance between flame performance and the mechanical properties of the compound.
- Particle size and distribution — uniform distribution in the matrix drives both dispersion during compounding and the consistency of the flame result.
- Compatibility — interaction with stabilisers, plasticisers, processing aids and any synergist already in the formulation.
- Processing window — barrel temperature, screw speed and residence time, set so that neither the flame retardant nor the polymer matrix degrades.
- Mechanical impact — tensile strength, impact resistance and flexural modulus after addition, and how much loss the part can tolerate.
- Heat stability — retention of properties in applications that see elevated service temperature.
- Surface appearance — specks, flow lines and colour consistency in visible parts.
- Compliance target — the flame rating and the environmental directives the finished article must satisfy.
Surface Modification, Dispersion and Appearance Control
We hold our own MCA surface modification technology, developed to solve the two problems that most often limit MCA in production: difficult dispersion and black and white specks in the finished part. Poor dispersion shows up twice — as visible defects on the surface and as localised areas where the flame retardant is not doing its job. Treating the particle surface changes how the powder wets into the melt and how it distributes through the screw, which stabilises both appearance and flame performance run to run.
The XS-MC series is used across wire and cable, electronic appliances, building materials and textile coatings, and the same surface treatment logic applies whether the carrier is a polyamide compound, a rubber formulation or a coating system.
Capacity, Quality Management and Compliance Evidence
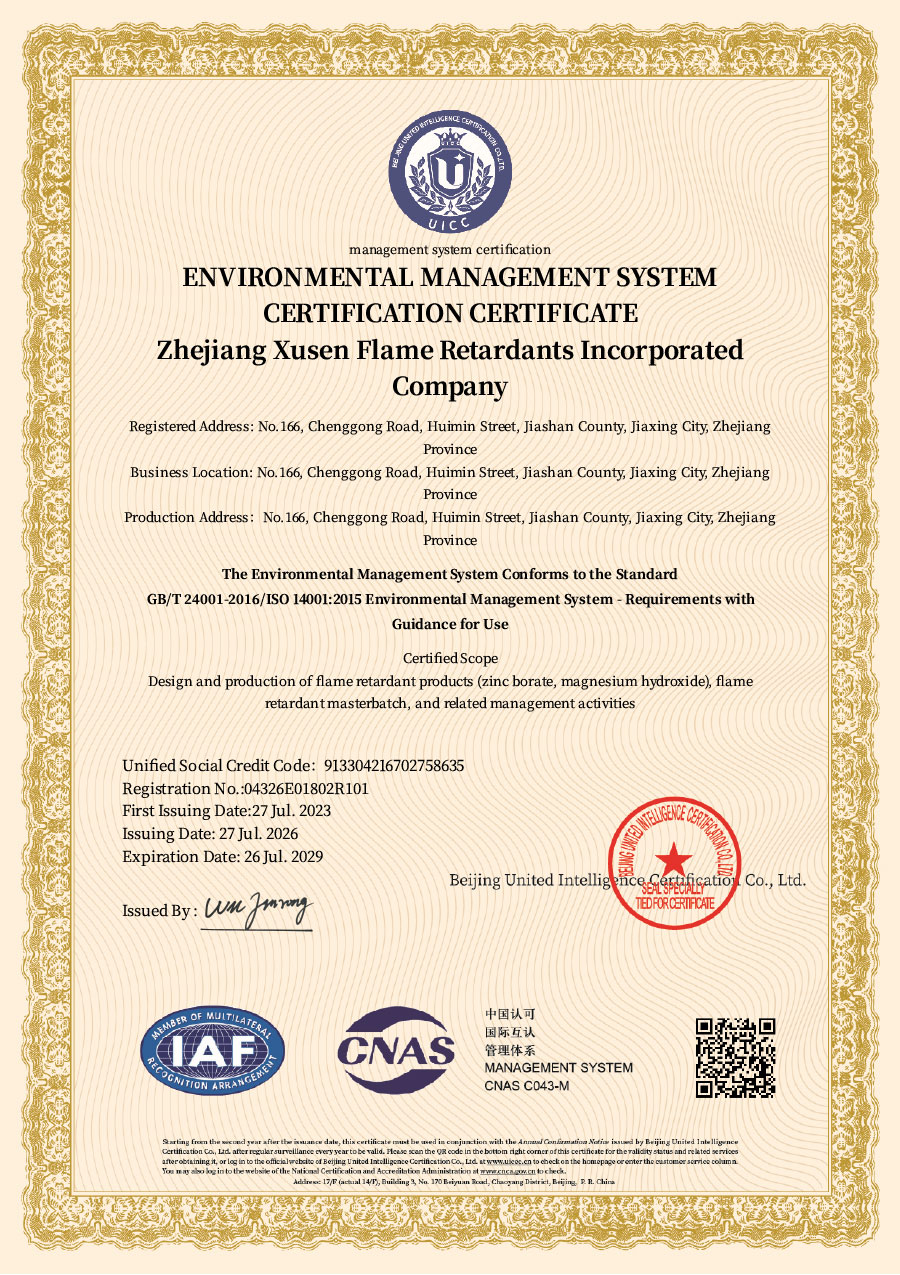
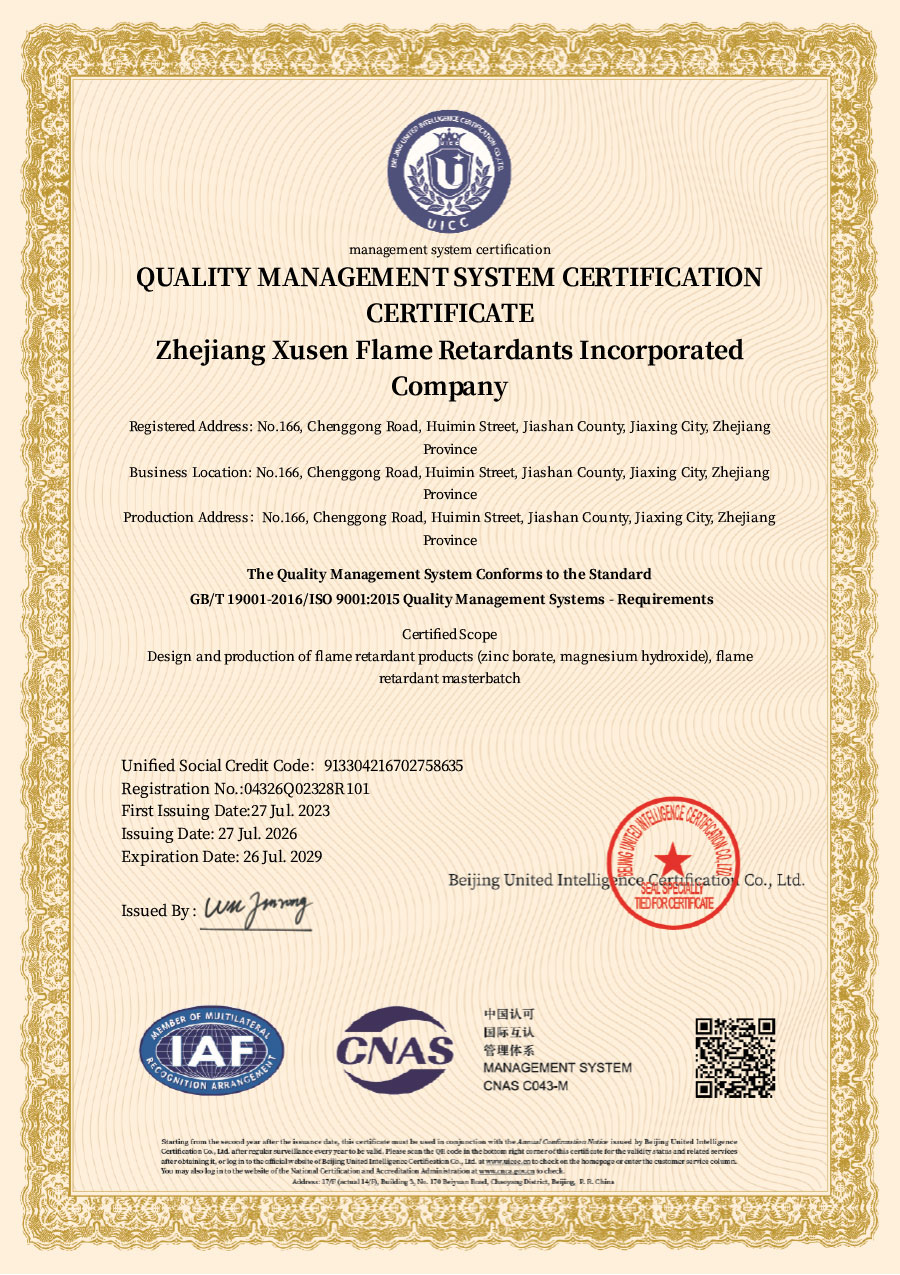
Production runs from two bases, Jiashan in Zhejiang and Juancheng in Shandong, with a current annual production capacity of 12,000 tons that continues to expand. Both sites operate their own production workshops and warehouses with complete production and quality inspection equipment, and every step of the product formation process follows the ISO 9001-2015 quality management system standard.
Our Zhejiang provincial-level scientific research laboratory works alongside a joint laboratory established with the Shanghai Institute of Chemistry for advanced flame-retardant materials. Together with Beijing Technology and Business University, Shandong Haihuai Institute and Shandong Brothers, we established China's advanced light industry flame retardant engineering technology research centre. We hold a number of invention and utility model patents and have participated in the formulation of national and industry standards.
All our products comply with the requirements of the WEEE, RoHS and EUP directives, and our MCA grades are REACH registered. MCA-specific documentation available with a quotation includes the MCA Halogen Test Report, the MCA RoHS 3.0 Test Report and the MCA RoHS Test Report, so that the compliance file for the finished article can be assembled without a separate testing round.
Information We Use to Configure Your Solution
Our proposal is built on the working point, the material and the production target. The matrix below shows what we ask for and what it determines.
| Project input | What it determines |
|---|---|
| Base polymer and grade, filler content, existing additive package | Series selection (XS-MC-15 or XS-MC-10/25/50) and whether a synergist is required |
| Target flame rating, test standard and specimen thickness | Loading window and the acceptance test agreed for the trial lot |
| Compounding or processing route: twin-screw, extrusion line, coating line, calendar | Particle size target, surface treatment choice and feeding arrangement |
| Mechanical property limits and appearance requirements | Upper bound on loading and the dispersion specification |
| Compliance file needed for the end product | Which test reports and declarations accompany the shipment |
| Packaging format, handling equipment and annual volume | Packaging, labelling and delivery scheduling |
Packaging, Delivery and Technical Support
Packaging format, net weight and labelling are confirmed against the grade and the receiving plant's handling equipment at the quotation stage, so that the material arrives in a form the line can actually feed. Alongside the material we provide process and technical support: guidance on loading, feeding position and processing window, and joint work on the formulation when the first trial does not land on the target rating.
For teams building a full halogen-free system rather than a single-substance addition, our wider range covers composite flame retardants, flame retardant masterbatch and functional additives, which allows the flame retardant package to be coordinated with the other additives in the compound instead of being sourced separately.
Frequently Asked Questions
What exactly is melamine cyanurate and what is its CAS number?
Melamine cyanurate is the 1:1 adduct of melamine and cyanuric acid, CAS 37640-57-6, molecular formula C6H9N9O3. It is a white crystalline powder, typically 1–5 μm, weakly acidic, practically insoluble in water and soluble in ethanol and formaldehyde. It is a nitrogen-based, high-efficiency halogen-free flame retardant with good chemical and thermal stability.
What is the difference between the XS-MC-15 and XS-MC-10/25/50 series?
The difference is the synthesis route. The XS-MC-15 Series is produced by a wet synthesis route, and the XS-MC-10/25/50 Series by a dry synthesis route. Both are REACH registered and both can be supplied with our surface modification treatment. The choice between them follows the polymer, the processing route and the appearance requirement of the finished part.
Can MCA replace a brominated flame retardant in polyamide?
In many application fields it can. MCA works through gas-phase dilution and foam-layer formation rather than halogen radical chemistry, so it avoids the smoke corrosivity and toxicity profile of brominated systems and is more environmentally friendly and safer. The trade-off is a higher loading and a check on mechanical properties, which we work through with you at the trial stage.
Which polymers is MCA best suited to?
Polyamide (PA6, PA66) and PBT are the strongest fits because the polymer itself contributes the char. In PP, rubber, cable compounds, adhesives, coatings and fabric backcoatings, MCA is used successfully but normally with a phosphorus-nitrogen or char-forming partner in the formulation.
Does MCA need a synergist in glass-fibre reinforced polyamide?
Often yes. Glass fibre changes both the burning behaviour and the char structure, and MCA alone may not reach the target rating. In those formulations we propose a composite flame retardant system for PA built around MCA chemistry, which is developed and produced in the same plant.
What compliance documentation is available for your MCA grades?
Our products comply with the WEEE, RoHS and EUP directives and our MCA grades are REACH registered. MCA-specific documents include the MCA Halogen Test Report, the MCA RoHS 3.0 Test Report and the MCA RoHS Test Report. Production follows the ISO 9001-2015 quality management system standard at both the Jiashan and Juancheng bases.
Related Products and Categories
Our portfolio also includes Products for applications with different operating ranges, interfaces or integration requirements.