

 English
 عربى
 简体中文
 +86-0573-89103923 / +86 182 6841 1181
Zhejiang Xusen Flame Retardants Incorporated Company has concentrated on halogen-free flame retardancy since 1997, and polyamide is one of the material families we build for. The PA range is a composite rather than a single salt, because unfilled, toughened and glass-fibre reinforced nylon each fail differently in a fire test and each needs a different balance of acid source, char former and gas-phase activity.
As a Composite flame retardant for PA manufacturer, we adapt the formulation to the polymer grade, the filler level and the processing window of the line it will run on. The XS-FR-3300 Series is the core product, and the same chemistry is also available in pellet form for let-down at the machine.
What the PA Range Covers
We supply the polyamide-relevant part of a wider halogen-free portfolio that also includes composite flame retardants for PP and polyester, single-substance flame retardants, masterbatches and functional additives. Within PA, the working range is:
- XS-FR-3300 Series halogen-free flame retardant for PA — the primary composite system for PA6 and PA66, including toughened and fibre-modified grades.
- flame retardant masterbatch for PA — the same chemistry in pellet form for dilution during compounding or at the injection machine.
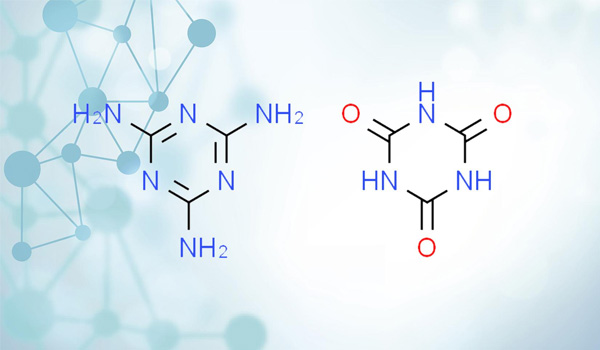
- Melamine cyanurate (MCA) — nitrogen-rich component used in unfilled PA and as part of composite systems.
- Ammonium polyphosphate (APP) — high-polymerisation and surface-modified grades that act as the acid source in intumescent systems.
- Functional additives for PA — stabilisers and processing aids used alongside the flame retardant to protect melt stability and surface quality.
Because the components are produced in-house, a formulation can be rebalanced rather than replaced when a project moves from a trial batch to a production compound.
XS-FR-3300 Series at a Glance
| Product family | Form | Role in a PA compound | Typical use |
|---|---|---|---|
| XS-FR-3300 Series | Powder | Phosphorus–nitrogen composite; primary halogen-free flame retardant system | Unfilled, toughened and glass-fibre reinforced PA6 / PA66 |
| Flame retardant masterbatch for PA | Pellet | Pre-dispersed let-down form | Lines without powder dosing, or final adjustment at the machine |
| Melamine cyanurate (MCA) | Powder | Nitrogen-based component; char promotion | Unfilled PA6 / PA66 and as a synergist in composite systems |
| Ammonium polyphosphate (APP) | Powder | Acid source in intumescent systems | Glass-fibre reinforced PA and compounds where char formation is required |
| Functional additives for PA | Powder or masterbatch | Stabilisers, processing aids and property modifiers | Compounds where heat stability or surface quality must be held |
Matching the System to the PA Grade
Nylon burns with dripping and little residual char, so the mechanism has to be chosen for the specific compound. Three cases cover most projects.
Unfilled PA6 and PA66
Unfilled grades respond well to nitrogen-rich chemistry, where the melt drips away from the flame and the additive promotes char at the surface. Loading is set by the wall thickness of the part and the rating required, and the main trade-off is elongation rather than tensile strength.
Toughened PA
Impact modifiers change melt rheology and can carry the flame retardant away from the burning surface. We adjust the ratio of acid source to char former so the system still forms a coherent char in a rubber-modified matrix, and we check that notched impact stays within the project target.
Glass-fibre reinforced PA
Glass fibre wicks heat and holds the polymer in place, which suppresses dripping and makes intumescent phosphorus–nitrogen chemistry the more effective route. Fibre loading, coupling agent and the fibre length retained after compounding all shift the required loading, so the recommendation is made against the actual reinforced compound rather than a generic PA.
Behaviour in Compounding and Moulding
Composite flame retardants for PA are hygroscopic to differing degrees, and moisture is the most common cause of a failed trial. The XS-FR-3300 Series should be stored in a cool, dry place and used soon after the bag is opened; if it has been stored for a period before use, we recommend baking at 90 °C for two hours.
- Dosing: powder systems feed best through a side feeder or a gravimetric loss-in-weight unit; masterbatch is dosed with the resin.
- Dispersion: medium shear with a dispersive mixing section, avoiding melt temperatures that pre-degrade the additive.
- Venting: vacuum venting removes volatiles and reduces surface defects such as silver streaks.
- Temperature: hold the melt within the window agreed for the grade; PA6 and PA66 run at different set points.
- Tooling: halogen-free systems avoid the hydrogen halide release that corrodes screws and moulds in halogenated formulations.
- Colour: the phosphorus–nitrogen system is white to off-white, so light and natural shades remain achievable.
Specifications We Fix for the PA Grade
The specification sheet issued with the PA grade fixes the parameters that govern performance and reproducibility in a nylon compound:
- Appearance and whiteness
- Phosphorus and nitrogen content
- Moisture content
- Particle size distribution and bulk density
- Water solubility and pH
- Thermal stability and decomposition onset
- Halogen content, confirmed by test report
Recommended loadings are empirical starting points. They are set against the equipment, raw materials and process of the user, and are adjusted together with the customer rather than treated as acceptance criteria.
Manufacturing, Quality System and Compliance Evidence
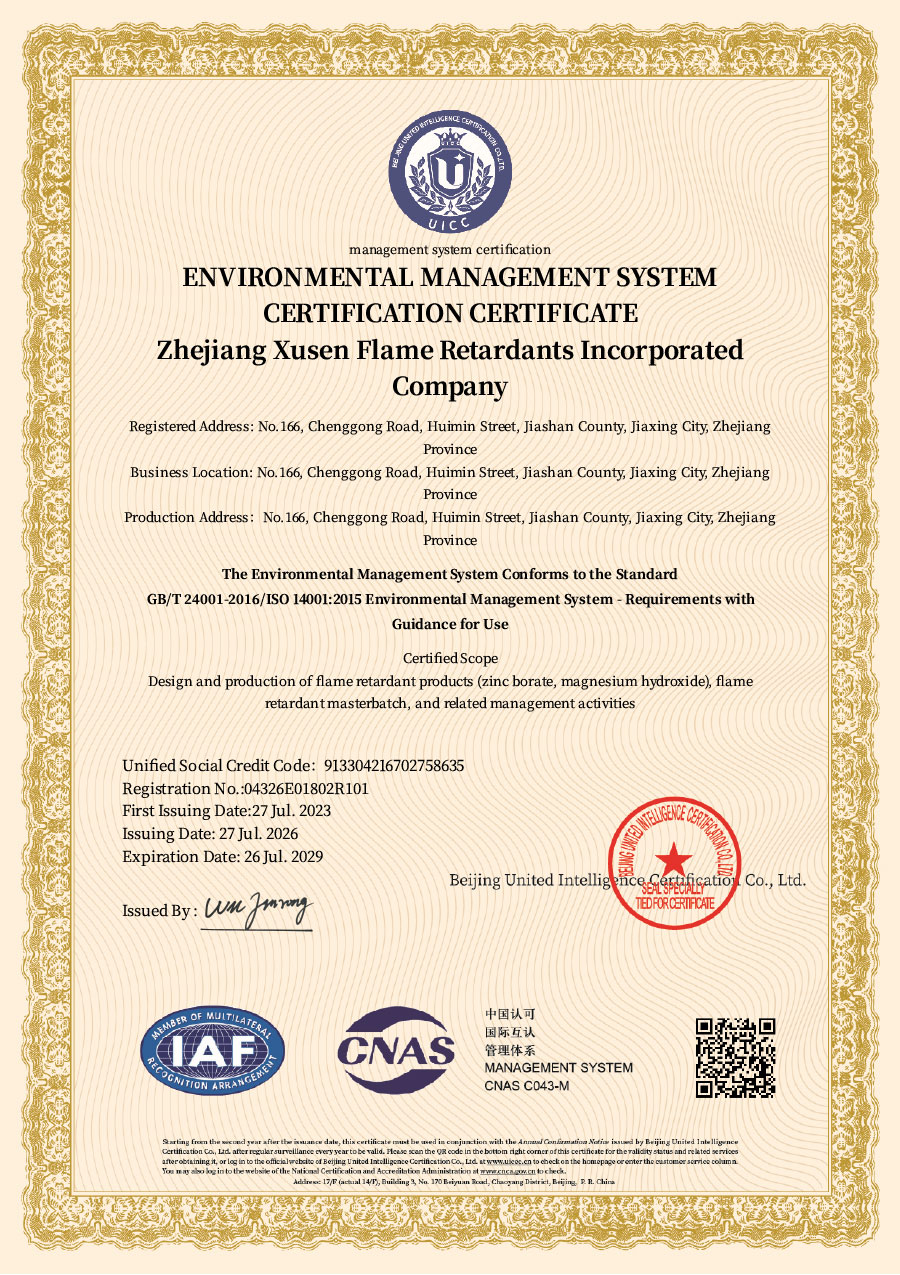
Production runs from two bases in China — Jiashan in Zhejiang and Juancheng in Shandong — with a combined annual capacity of 12,000 tons that continues to expand. Both sites operate production workshops and warehouses with in-house production and inspection equipment, and every step follows the ISO 9001-2015 quality management system.
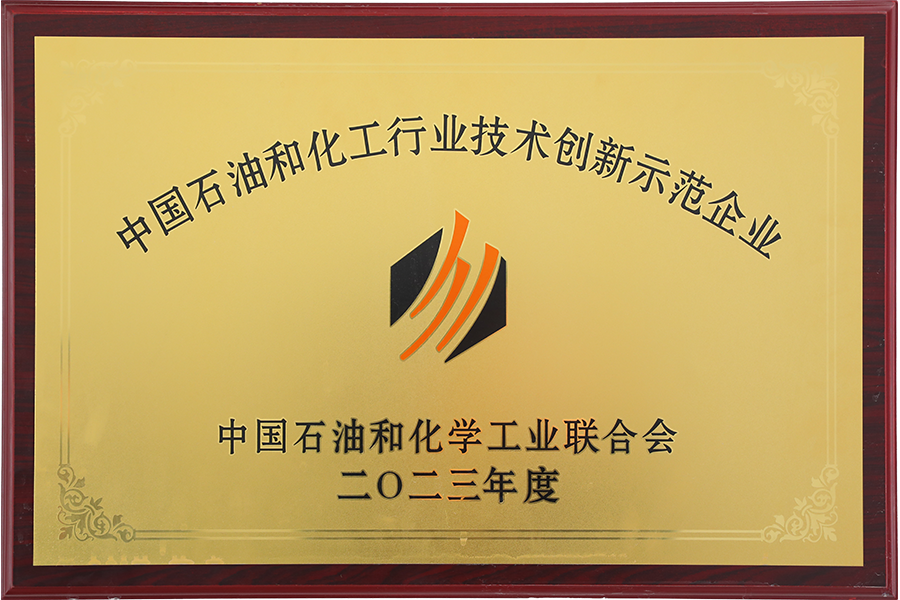
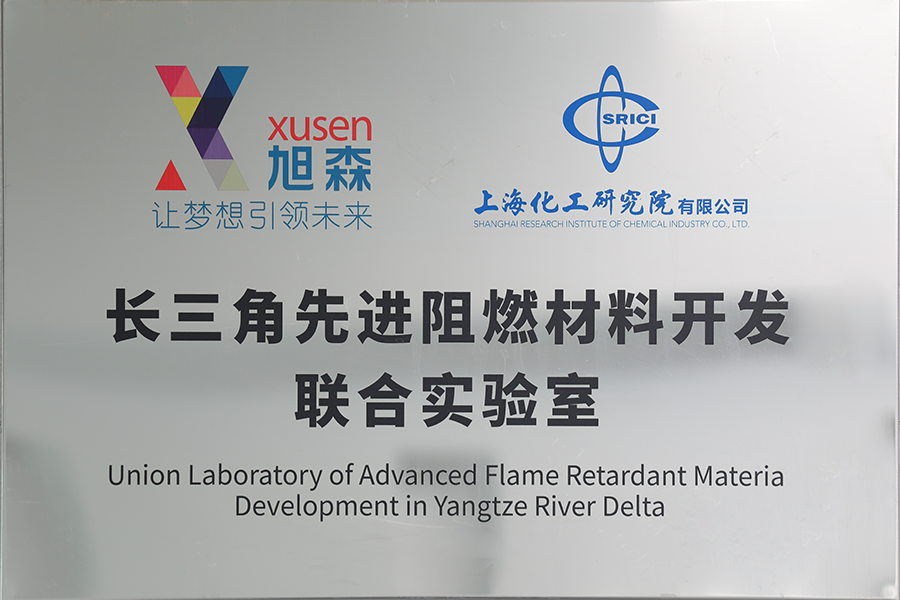
Development work is supported by a Zhejiang provincial-level scientific research laboratory, a joint laboratory with the Shanghai Institute of Chemistry, and a light industry flame retardant engineering technology research centre established with Beijing Technology and Business University, Shandong Haihuai Institute and Shandong Brothers. The company holds invention and utility model patents and has taken part in drafting national and industry standards.
Products comply with WEEE, RoHS, REACH and EUP requirements. A RoHS test report for flame retardant for PA is available, together with halogen test reports and MSDS documentation for the individual grades.
Adaptive Improvement, Packaging and Handling
We make adaptive improvements to the standard grades so that they fit a customer's process and product characteristics — a change in loading, surface treatment or particle size rather than a new chemistry. Requests are handled against the compound data the customer supplies.
- Packaging: 25 kg per bag, with grade and lot marked on the label.
- Shelf life: 12 months from production when stored as labelled.
- Storage: cool, dry and sealed; use promptly after opening, or bake at 90 °C for two hours.
- Handling: follow the protective measures in the MSDS and dispose of packaging to local environmental requirements.
Information We Use to Configure Your Solution
A configuration and quotation are prepared from the working point of the compound, not from a catalogue number alone. The following inputs let us set the system and the loading on the first proposal.
| Input | What we need | Why it changes the recommendation |
|---|---|---|
| Polymer | PA6 or PA66, viscosity grade, supplier | Melt temperature and crystallinity set the decomposition window |
| Filler and reinforcement | Type and percentage of glass fibre, mineral or none | Determines whether a dripping or an intumescent mechanism is used |
| Impact modifier | Type and level of toughener | Affects char coherence and the acid-to-char-former ratio |
| Target rating | Rating, test standard and specimen thickness | Thinner sections generally need a higher loading |
| Process | Compounding equipment, dosing method, melt temperatures, cycle time | Sets the powder or masterbatch form and the dispersion advice |
| Property targets | Tensile, elongation, impact, electrical and colour requirements | Defines how far the loading can be pushed |
| Market and volume | Destination market, regulatory scope, annual tonnage, packaging preference | Drives documentation, labelling and supply planning |
Questions We Are Asked About PA Flame Retardants
Which PA grades does the XS-FR-3300 Series suit?
PA6 and PA66, including toughened and glass-fibre reinforced compounds. The loading and the internal balance of the composite are set for the specific grade rather than applied as a fixed figure across the family.
What flame retardancy rating can be targeted?
The series is designed for UL-94 V-0 at the recommended loading in suitable PA compounds. The result depends on wall thickness, fibre content and the rest of the formulation, so it is confirmed on the customer's own compound.
Does the flame retardant affect mechanical properties?
Any additive changes the balance. In unfilled PA the main effect is on elongation; in reinforced grades the fibre carries most of the load. We adjust the system to hold the properties the finished part needs.
Is a masterbatch available instead of powder?
Yes. Flame retardant masterbatch for PA carries the same chemistry in pellet form for let-down during compounding or at the injection machine, which suits plants without powder dosing equipment.
What documentation is supplied with a grade?
Specification sheet, MSDS, halogen and RoHS test reports for the relevant grade, and packaging labels carrying grade, lot and shelf-life information.