

 English
 عربى
 简体中文
 +86-0573-89103923 / +86 182 6841 1181
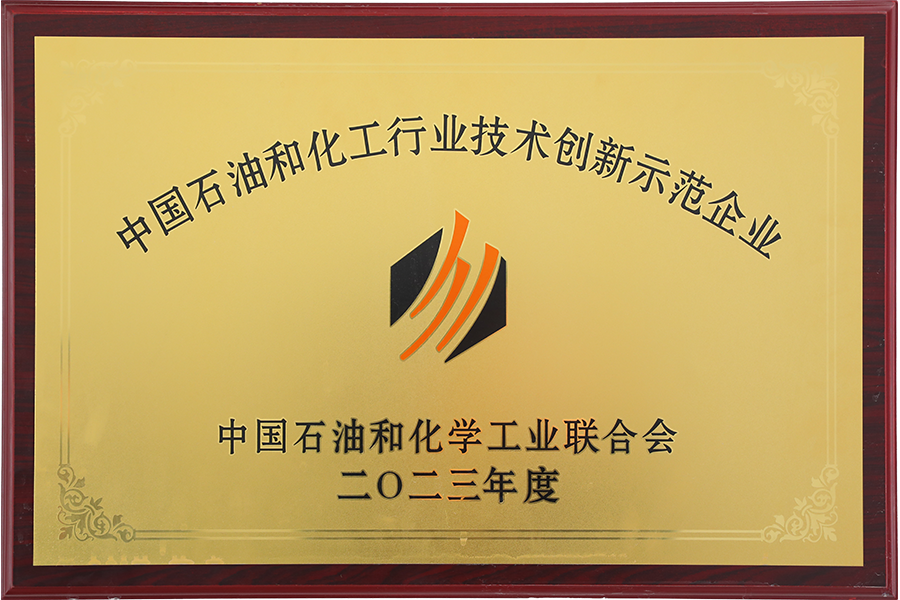
Zhejiang Xusen Flame Retardants Incorporated Company produces halogen-free flame retardants from two production bases in Jiashan, Zhejiang and Juancheng, Shandong, with an annual capacity of 12,000 tons. Aluminum hydroxide (ATH) is one of our core single-substance lines, supplied as a mineral flame retardant and smoke suppressant for cable compounds, adhesives, rubber, composites and other polymer systems where halogen-free performance and low smoke output are the governing requirements.
- Chemistry: Al(OH)3, CAS 21645-51-2 — a mineral hydroxide, not a halogenated or phosphorus-based additive.
- Supply routes: screened base ATH and surface-treated modified ATH, selected by particle size and crystal form.
- Positioning: a China ATH manufacturer working from mineral feedstock through surface treatment to application-matched grades.
The Aluminum Hydroxide (ATH) Range We Manufacture
Our ATH portfolio is organised around two supply routes. The Aluminum Hydroxide XS-ACW Series covers grades screened by particle size and crystal form for the application in question. The Modified ATH Series adds surface treatment so the filler behaves better inside the polymer matrix.
| Grade family | Treatment | Engineering purpose | Typical fit |
|---|---|---|---|
| Aluminum Hydroxide XS-ACW Series | Screened by particle size and crystal form | Endothermic water release, smoke suppression, char promotion | Cable compounds, adhesives, composites |
| Modified ATH Series | Surface treated | Improved substrate compatibility, better dispersion, resistance to settling and stratification | Wire and cable, adhesives, filled composites |
Both routes sit inside our broader Single-substance flame retardants programme, which also covers MCA, ammonium polyphosphate and organophosphorus chemistries. Where a formulation needs a combined effect rather than a single mineral filler, ATH is frequently paired with those systems or delivered through our masterbatch route.
How ATH Behaves in a Burning Polymer
Aluminum hydroxide decomposes on heating and releases its crystal water in a strongly endothermic reaction. That reaction absorbs a large amount of heat and cools the polymer surface, while the water vapour dilutes the combustible gases feeding the flame. The residue promotes carbonisation rather than dripping, and because the filler is non-volatile it stays in the matrix instead of migrating out.
- No toxic gases are generated at high temperature, and smoke density in the burning polymer is reduced.
- The additive is non-toxic and chemically stable, which suits long-service cable and construction parts.
- Because decomposition begins well below the processing window of high-temperature engineering plastics, ATH is normally specified for polyolefins, elastomers, adhesives and thermosets rather than for high-melt nylons.
Application Fit Across Polymers and Processes
ATH is a high-loading filler, so the grade has to be matched to the carrier system as carefully as the flame test itself. The matrix below shows where the two families typically land and what we confirm before a grade is released for a trial.
| System | Why ATH fits | What we confirm |
|---|---|---|
| EVA and cable compounds | Low-smoke, halogen-free insulation and sheathing; endothermic cooling limits drip | Loading level, particle size cut, surface treatment, extrusion temperature ceiling |
| PP and TPE elastomers | Mineral route avoids halogenated systems in moulded and extruded parts | Dispersion quality, impact retention, colour and surface finish |
| Adhesives and sealants | Stable in the binder, non-volatile, does not migrate out of the cured joint | Settling and stratification behaviour, viscosity build, cure compatibility |
| Rubber and TPE compounds | Thermal stability through vulcanisation, smoke reduction | Moisture content, pH, cure system interaction |
| Epoxy and thermoset composites | Filler loading without halogen, char promotion in the resin | Treatment chemistry matched to resin polarity, wet-out, sedimentation |
| Coatings, carpet backing and fabric coating | Fine particle fractions for thin films, low smoke in textile applications | Top cut, sieve residue, rheology in the coating paste |
Specifications That Drive Grade Selection
Two ATH grades with the same chemistry can behave completely differently on a line. These are the parameters that decide which cut and treatment we propose, and the values we confirm for the grade actually supplied.
- Particle size distribution — median size and top cut govern dispersion, surface finish and mechanical loss at high loading.
- Crystal form — screened alongside particle size because it affects packing and processing behaviour.
- Surface treatment type and level — the single biggest lever on compatibility, wet-out and settling.
- Moisture content — critical for adhesives, epoxy and any system sensitive to voids or pre-cure.
- Colour and whiteness — relevant for natural, light or pigmented compounds.
- pH and conductivity — relevant where electrical performance of the insulation compound is specified.
- Oil absorption and bulk handling — sets the practical loading ceiling and feeding behaviour on the compounding line.
Surface Treatment, Dispersion and Processing Behaviour
Untreated mineral filler in a non-polar polymer tends to agglomerate, and in liquid systems it settles and stratifies over time. Our modified ATH grades are surface treated to raise compatibility with the substrate and improve dispersion, which is what keeps the filler evenly distributed through the compound and through the shelf life of an adhesive or sealant.
Treatment chemistry is selected against the polarity of the carrier system and the process it will see. A treatment that performs well in an epoxy composite is not automatically the right choice for an EVA cable compound, so we treat the treatment route as a configuration decision rather than a catalogue default. Surface treatment technology is one of the four technical pillars behind our ATH and composite lines, alongside synthesis, composite formulation and masterbatch manufacturing.
Capacity, Quality Control and Compliance Evidence
Production runs across two bases — Jiashan in Zhejiang and Juancheng in Shandong — with a current annual capacity of 12,000 tons that continues to expand. Both sites operate their own workshops and warehouses with complete production and quality inspection equipment, and every step of product formation follows the ISO 9001-2015 quality management system standard.
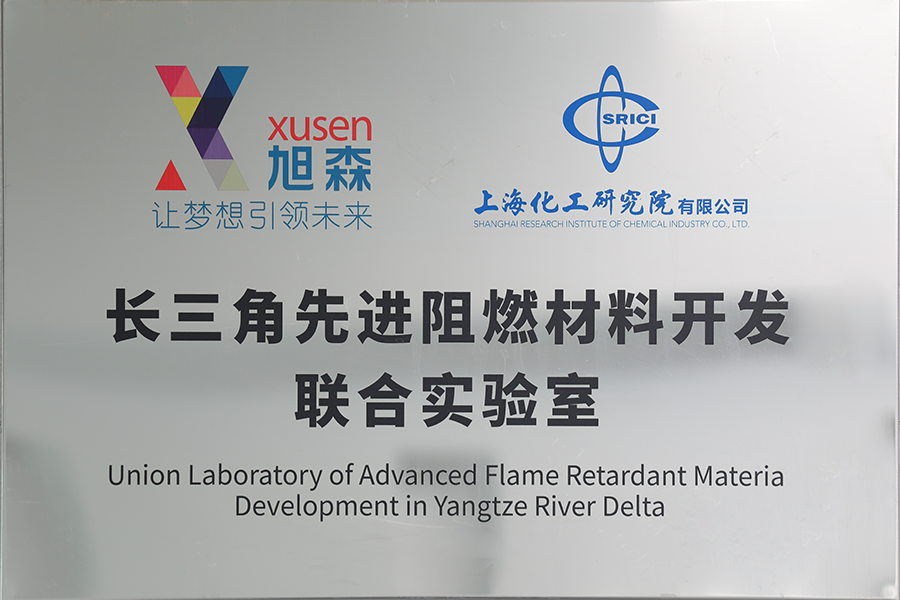
Technical work is supported by our Zhejiang provincial-level scientific research laboratory, a joint laboratory with the Shanghai Institute of Chemistry for advanced flame-retardant materials, and a light industry flame retardant engineering technology research centre established with Beijing Technology and Business University, Shandong Haihuai Institute and Shandong Brothers. We hold a number of invention and utility model patents and have participated in the formulation of national and industry standards.
Compliance position for ATH:
- Our products comply with the requirements of the WEEE, RoHS and EUP directives.
- An ATH RoHS test report is available as supporting documentation for qualification files.
Customization, Packaging and Delivery Scope
Because ATH performance is set by physical form as much as by chemistry, most projects need a grade that is configured rather than picked off a shelf. We work on particle size cut, crystal form selection, surface treatment route and moisture control, and we can supply ATH as a standalone single-substance product or as part of a composite or masterbatch system where the formulation calls for it.
Packaging format, net weight, palletisation and labelling are agreed with the order so that the material arrives in a form your intake and dosing equipment can handle. Delivery scope, documentation set and shipping terms are confirmed in the quotation, and we coordinate the logistics of domestic and international shipments so that documentation and customs requirements are met before dispatch.
Information We Use to Configure Your Solution
A configuration and quotation for ATH is only as good as the working point behind it. The following inputs let us propose a specific grade, treatment and packaging rather than a generic mineral filler.
| Project input | Why we need it |
|---|---|
| Polymer or binder system and target filler loading | Sets the compatibility requirement and the practical loading ceiling |
| Processing window — maximum melt temperature and residence time | Keeps the compound below the decomposition onset of the filler |
| Target flame test and standard | Determines whether ATH alone is sufficient or a composite route is needed |
| Smoke density and toxicity requirements | Confirms the smoke-suppression role the filler has to play |
| Particle size and dispersion target | Drives the size cut, top cut and treatment selection |
| End-product form — cable, adhesive, sheet, coating or moulded part | Aligns rheology, surface finish and mechanical expectations |
| Volume, delivery schedule and packaging preference | Matches production planning to the two-base capacity |
| Documentation set required | Defines the test reports and technical data issued with the shipment |
Frequently Asked Questions
What is the difference between the XS-ACW Series and the Modified ATH Series?
The XS-ACW Series is screened by particle size and crystal form for the intended application. The Modified ATH Series goes a step further with surface treatment, which raises compatibility with the substrate, improves dispersion and reduces settling and stratification. Choose the modified route when dispersion quality or shelf stability is the limiting factor.
Which polymers can be flame retarded with Aluminum hydroxide (ATH)?
ATH is used in adhesives, wire and cable compounds and composite materials, and it fits polyolefin systems, TPE elastomers, rubber, epoxy and other thermosets, coatings and textile coating applications. It is not the right choice for polymers processed well above the filler's decomposition onset, where a different halogen-free chemistry is required.
Why does ATH need such high loading, and what does that do to mechanical properties?
The flame-retardant effect comes from the endothermic release of crystal water, so a substantial volume fraction of filler is needed to cool the polymer and dilute the combustible gases. High loading raises viscosity and can reduce elongation and impact strength, which is why particle size cut and surface treatment matter — they let you reach the required loading with better dispersion and less mechanical penalty.
Does ATH suppress smoke as well as flame?
Yes. The water vapour released during decomposition dilutes combustible gases, the residue promotes carbonisation rather than dripping, and smoke density in the burning polymer is reduced. The filler is non-volatile and does not precipitate, so it stays in the matrix for the service life of the part.
What documentation is available for ATH grades?
An ATH RoHS test report is available, and our products comply with the WEEE, RoHS and EUP directives. The documentation set issued with a shipment is agreed at quotation stage so that it matches your qualification and intake requirements.
Can you supply ATH matched to a specific particle size or surface treatment?
Yes. Particle size, crystal form and surface treatment are configuration variables in our ATH range, and we also supply the material through composite and masterbatch routes when the formulation calls for a combined effect. Send us the working point, the target flame test and the end-product form, and we will propose the grade, treatment and packaging that fit.